dgfeman com's Store
Owned by dgfeman com Joined Sep 2023 8 Listings
dgfeman com's Store
easyid.me/biz/dgfeman-6af120 • Verified Store
Scan to open official EasyID digital store, view live catalog, or save business card.
Verified Merchant
EasyID Certified Seller
Fast 24h Packing
Direct courier dispatch
Zero Escrow Direct
Direct merchant settlement
Store Listings (2)
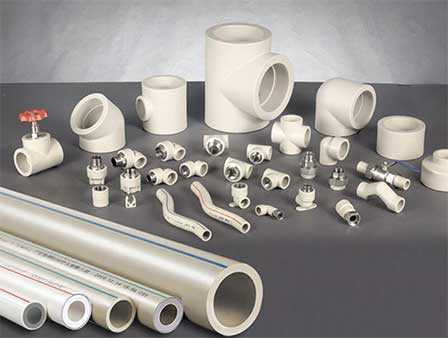
Several Common Problems and Solutions of Plastic Injection Parts
Ⅰ. Reasons and solutions for deformation of plastic injection parts <br> <br>An injection molded part is shaped like a cavity but is a twisted version of the cavity shape. <br> <br>1. Possible reasons for the problem <br> <br>(1) Bending is due to excessive internal stress in the injection molded part. <br> <br>(2) The mold filling speed is slow. <br> <br>(3) Insufficient plastic in the mold cavity. <br> <br>(4) The plastic temperature is too low or inconsistent. <br> <br>(5) The plastic injection parts are too hot when ejected. <br> <br>(6) Insufficient cooling or inconsistent temperature of moving and fixed molds. <br> <br>(7) The structure of the plastic injection parts is unreasonable (for example, the reinforcing ribs are concentrated on one side, but far apart). <br> <br>2. Remedy <br> <br>(1) Reduce the injection pressure. <br> <br>(2) Reduce the forward time of the screw. <br> <br>(3) Increase cycle time (especially cooling time). Immerse in warm water (38°C) immediately after ejection from the mold (especially thicker plastic injection parts) to slowly cool the plastic injection parts. <br> <br>(4) Increase the injection speed. <br> <br>(5) Increase the plastic temperature. <br> <br>(6) Use cooling equipment. <br> <br>(7) Appropriately increase the cooling time or improve the cooling conditions to ensure that the mold temperatures of the movable and fixed molds are consistent as much as possible. <br> <br>(8) Improve the structure of plastic parts according to the actual situation where permitted. <br> <br>Ⅱ. Common problems that should be paid attention to in the injection molding process of transparent plastic injection parts <br> <br>Due to the high light transmittance of transparent plastics, the surface quality of plastic products must be strictly required, and there should be no defects such as streaks, pores, whitening, halo, black spots, discoloration, and poor gloss. Equipment, molds, and even product design, must pay great attention and put forward strict or even special requirements. <br> <br>Secondly, since most of the transparent plastics have high melting point and poor fluidity, in order to ensure the surface quality of the product, a higher temperature is often required, and the process parameters such as injection pressure and injection speed should also be finely adjusted, so that the plastic injection can be filled with the mold, It will not generate internal stress and cause product deformation and cracking. <br> <br>Therefore, strict operation should be carried out in terms of raw material preparation, equipment and mold requirements, injection molding process and raw material processing of products. Here are some types of plastic material for injection molding. <br> <br>Ⅲ. Common problems of color difference control of plastic molded products <br> <br>Chromatic aberration is a common defect in injection molding. There are many factors affecting color difference, involving raw resin, color masterbatch, mixing of color masterbatch and raw materials, injection molding process, injection molding machine, etc. <br> <br>Ⅳ. Adjust the process parameters of plastic injection parts(temperature/pressure/speed/position) <br> <br>The measurement and control of temperature is very important in plastic injection moulding services. While making these measurements is relatively simple, most injection molding machines do not have sufficient temperature pick-up points or lines. On most injection molding machines, the temperature is sensed by a thermocouple. A thermocouple basically consists of two different wire tails joined together. If one end is hotter than the other, a tiny electrical signal will be generated; the more heated, the stronger the signal. <br> <br>As one of injection mold suppliers china, we will do our best to meet all the needs of customers.
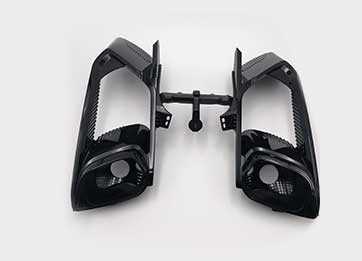
Common Quality Problems of Plastic Injection Parts
After injection molding, there are some bad problems, which will affect the assembly efficiency or the performance of the whole machine. There are certain differences with the predetermined quality standards (inspection standards), which cannot meet the company's quality requirements. In addition to strengthening the quality awareness training of employees and dealing with defective parts in a timely manner (such as selection, processing, etc.); these defects may be caused by the following aspects: molds, raw materials, process parameters, equipment, environment, and personnel. The defects are summarized as follows: <br> <br>1. Color difference of plastic injection parts <br> <br>The color of the injection molded part is different from the single standard color sample when viewed with the naked eye, and it is judged as a color difference under the standard light source. <br> <br>2. The plastic injection parts are not satisfied (lack of glue) <br> <br>Usually lack of glue refers to the uneven flow of glue, that is, the cavity is not full. The plastic moulding parts are not full, and there are bubbles, voids, shrinkage holes, etc., which do not match the standard model, which can also be called lack of glue. <br> <br>3. Warpage and deformation of plastic injection parts <br> <br>The shape of the injection molded part is rotated and twisted after the plastic part is demolded or for a period of time. If the straight edge is facing inward, or the flat part is curved outward, or the flat part has undulations, there are local and overall deformation. <br> <br>4. Welding line (pattern) of plastic injection parts <br> <br>The linear traces on the surface of the plastic injection parts are formed by the fusion of plastics in the mold, and the melts are not completely fused together at the intersection. Deep to shallow development, this phenomenon has a certain impact on the appearance and mechanical properties. Such as the weld line at the bottom of the hook plate. <br> <br>5. Corrugation of plastic injection parts <br> <br>The surface of the plastic injection parts has a spiral or cloudy wave-like uneven phenomenon, or there are corrugated lines on the inside of the transparent products, which are called corrugations. <br> <br>6. Overfill of plastic injection parts (flash, drape) <br> <br>A thin (flash) compound appears around the parting line around the injection molded part or on the sealing surface of the mold, which is called overflow. <br> <br>7. Silver thread pattern of plastic injection parts <br> <br>The long, needle-like silver-white frost-like fine lines on the surface of the plastic injection parts, the opening direction is along the direction of the material flow, and the front end of the fluid is rough where the plastic parts are not completely filled, called silver lines (silver lines) . <br> <br>8. Uneven color of plastic injection parts (color mixing) <br> <br>The color of the surface of the plastic injection parts is not uniform, there are shades and different hues, which is called color mixing. <br> <br>9. Poor gloss of plastic injection parts (dark color) <br> <br>The surface of the injection molded part is dull and dull or the gloss is uneven, which is called dark color or poor gloss. <br> <br>10. Poor demoulding (deformation from demoulding) <br> <br>Similar to warpage deformation, the plastic injection parts cannot be released from the mold smoothly after molding, and there are deformations, white tops, cracks, strains, etc., which are called poor demoulding. <br> <br>11. Cracks and ruptures of plastic injection parts <br> <br>Void cracks and resulting breakage appear on the surface of the injection molded part. <br> <br>12. Foaming (burning) of plastic injection parts <br> <br>Many dark black streaks or black spots appear on the surface or inside of the plastic injection parts, which are called smears or burns. <br> <br>13. The size of the plastic injection parts does not match <br> <br>During the molding process of plastic injection parts, the failure to maintain the original predetermined dimensional accuracy is called dimensional non-conformity. <br> <br>14. Bubble and dark bubble in plastic injection parts <br> <br>There are pores inside the plastic injection parts. Bubble is the defect of small volume or a series of pores formed inside the product after molding, and dark bubble is the vacuum hole generated inside the plastic. <br> <br>15. Mixed corrosion on the surface of plastic injection parts <br> <br>The surface of the plastic injection parts presents a dull, whitish and hazy appearance, which is called mixed corrosion. <br> <br>16. Depression of plastic injection parts <br> <br>The surface of the plastic injection parts is uneven, smooth, and shallow pits or dimples are generated inward. <br> <br>17. Cold material for plastic injection parts (cold glue) <br> <br>The surface of the injection molded part is formed of cold glue, and the color, performance and body are all different plastics. <br> <br>18. Top white/top height of plastic injection parts <br> <br>The surface of the plastic injection parts is obviously white or higher than the original plane. <br> <br>19. White spot of plastic injection parts <br> <br>There are white particles in the plastic injection molding products, and the particles are also called "fish eyes", which are mostly reflected on the transparent products. <br> <br>20. Insufficient strength of plastic injection parts (brittle cracking) <br> <br>The strength of the injection molded part is lower than expected, so that the injection molded part cannot withstand the predetermined load. <br> <br>As a china plastic molding company, we will do our best to meet all the needs of customers.
About dgfeman com's Store
No description provided.
0.0
Customer Reviews
See what others are saying about dgfeman com's Store. We verify purchases to ensure reviews are genuine.
No reviews yet for this store.