dgfeman com's Store
Owned by dgfeman com Joined Sep 2023 8 Listings
dgfeman com's Store
easyid.me/biz/dgfeman-6af120 • Verified Store
Scan to open official EasyID digital store, view live catalog, or save business card.
Verified Merchant
EasyID Certified Seller
Fast 24h Packing
Direct courier dispatch
Zero Escrow Direct
Direct merchant settlement
Store Listings (2)
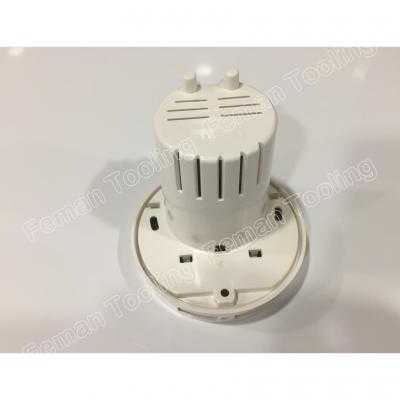
Several Parameters That Should Be Paid Attention to in the Injection Mold Design
There are two templates on the injection molding machine, one does not move, called fixed template; the other can move, called moving template. The mold is fixed on the two templates by screws and pressure plates respectively. When the mold is opened, the movable platen of the injection molding machine moves, thereby driving the mold to open. <br> <br>After the mold is manufactured, injection molding is carried out, the injection molding machine is loaded, and the product is started. However, there are many models of injection molding machines, and each injection molding machine has its own parameters. For plastic die maker in china, the injection mold design must be able to meet the requirements of the injection molding machine model provided by the customer, otherwise it will not be able to produce. <br> <br>There are many design parameters of the injection molding machine. The following focuses on several parameters related to the mold. <br> <br>1. Injection volume of injection mold design <br> <br>The injection volume is the maximum mass value (or volume value) of the melt that the injection molding machine can inject at one time during production, which represents the maximum injection capacity of this type of injection molding machine. The amount of melt used in the design of an injection mold is smaller than the injection volume of the injection molding machine. Otherwise, the product like insert molding electronics is dissatisfied and cannot be produced. <br> <br>2. Clamping force of injection mold design <br> <br>What is at stake is the pressing force of the injection molding machine on the template when the mold is closed. The clamping force required by the molded product during molding must be less than the rated clamping force of the selected injection molding machine. Otherwise, the melted glue will easily run away from the parting surface, resulting in flash. <br> <br>3. Tie rod spacing for injection mold design <br> <br>There are four tie rods in the dead corners of the fixed platen and the movable platen of the injection molding machine. Their function is to ensure that the injection molding machine has sufficient strength and rigidity, and at the same time is responsible for sliding the template. But it tends to limit the overall size of the mold, because the mold is installed from the middle of the tie rod. <br> <br>The dimensions of the mold cannot be larger than their corresponding tie rod spacing at the same time. If the length of the mold exceeds the tie rod spacing, check whether the mold is hoisted into the tie rod workshop by rotating. If the rotating hoisting cannot be carried out, only the mold size can be changed. , or replace the injection molding machine. <br> <br>4. Nozzle size check for injection mold design <br> <br>The nozzle head of the cheap injection molding machine is generally spherical. When selecting the sprue sleeve, the spherical radius of the sprue sleeve should be consistent with the spherical radius of the nozzle. In order to prevent the high-pressure melt from overflowing from the contact gap between the nozzle and the sprue sleeve, generally the ball radius of the sprue sleeve should be larger than the nozzle ball radius, and the size of the small end of the sprue should also be slightly larger than the size of the nozzle hole, so that the nozzle can be Sprue sleeves are easy to align. <br> <br>As a plastic mold tooling company, we will do our best to meet all the needs of customers.
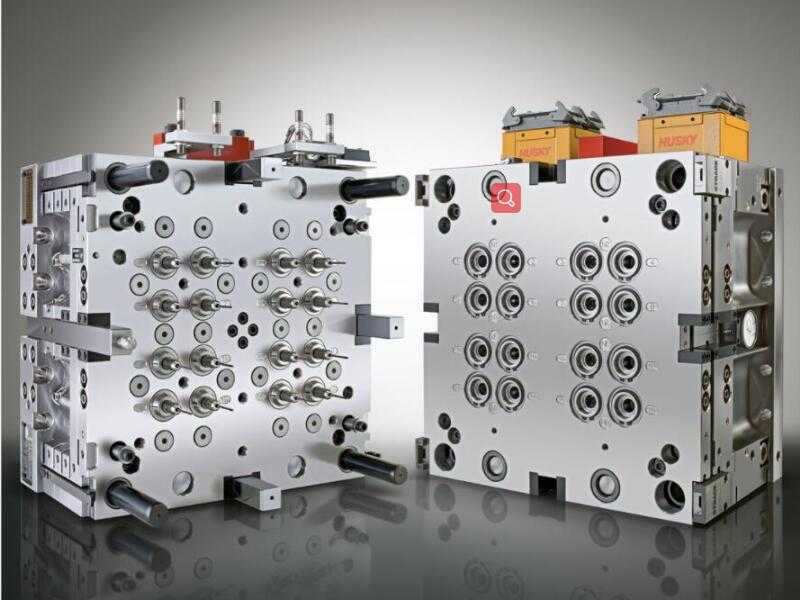
PP Injection Molding
Chromatic aberration of injection molded parts: a common problem between the casing and the appearance parts. <br> <br> <br>① Factors in raw materials: including toner replacement, plastic material grade change, and setting agent replacement. <br> <br>② Different types of raw materials: For example, injection molding polypropylene and ABS material or injection molding polycarbonate require the same color, but there is a slight color difference due to different material types, but a limited range is allowed. <br> <br>③ Equipment process reasons: <br> <br>A. temperature; <br> <br>B. Pressure; <br> <br>C melting time; <br> <br>D. Different batches of mixing materials, different machines and other process factors. <br> <br>④ Environmental factors: the barrel is not clean, the drying hopper is dusty, the mold is oily, etc. <br> <br>⑤ Factors of the toner itself: some toners are not affected by temperature, and the products are easily changed by temperature changes. <br> <br>2. Injection molding parts are not satisfied (lack of glue) <br> <br>Generally, the parts that appear are: deep, thin, long, thin, far from the gate, easy to trap air and lack of glue in places with debris in the mold. <br> <br>① Mould: <br> <br>A. The design of the gating system is unreasonable. The gating system is the channel for the melt to enter the mold cavity, which has a great relationship with the molding quality of the injection molded parts. The gate is not parallel, and the position of the gate is not in the wall thickness; <br> <br>B. The mold exhaust structure is poor; <br> <br>C. Impurities or cold materials in the melt block the flow channel; <br> <br>D. The mold temperature does not meet the requirements. <br> <br>② In terms of raw materials: <br> <br>A. The moisture content of raw materials is too large; <br> <br>B. The volatile matter in the raw material exceeds the standard; <br> <br>C. There are too many impurities or recycled materials in the raw materials. <br> <br>③ Injection molding machine: <br> <br>A. Insufficient injection volume: For example, a 150T machine is used to produce 180T products. <br> <br>B. The nozzle is blocked by foreign matter, and the nozzle hole is too small; <br> <br>C. Insufficient supply of raw materials: if the barrel is blocked, the nozzle material will affect the blanking; <br> <br>D. Check valve failure; <br> <br>E. The injection stroke is not enough; <br> <br>F. The sealing ring of the injection cylinder is damaged. <br> <br>④ Forming operation: <br> <br>A. The mold temperature is too low; <br> <br>B. The injection pressure is too low; <br> <br>C. The pressure holding time is too short; <br> <br>D. The injection speed is too slow or too fast; <br> <br>E. The melt temperature is too low. <br> <br>3. Warpage and deformation of injection molded parts <br> <br>① Mould: <br> <br>Mainly due to unreasonable reasons in mold design. <br> <br>② Forming operation: <br> <br>A. The injection pressure is too high, the molecular orientation of the fluid direction and the vertical flow direction are quite different, and the plastic tries to restore the original curled state, so the shrinkage in the fluid flow direction is greater than that in the vertical flow direction; <br> <br>B. The melt temperature is too high; <br> <br>C. The holding pressure is too high: when the holding pressure is high, the internal pressure in the plastic is too high, and the release of the internal stress after demolding causes the injection molded parts to warp and deform; <br> <br>D. The melt flow rate is too slow; <br> <br>E. The tempering temperature is too high or the time is too long. <br> <br>③ In terms of raw materials: PP/PA materials are easily deformed. <br> <br>4. Welding line (pattern) of injection molded parts <br> <br>① Mould: <br> <br>A. There are too many gates, that is, there are too many glue feeding points, and the cross-sectional area of the glue feeding mouth is too small; <br> <br>B. There is no cold material hole in the mold or the position of the cold material hole is incorrect; <br> <br>C. The design of the mold cooling system is unreasonable, and the melt is cooled too fast and unevenly in the mold. <br> <br>② In terms of raw materials: <br> <br>A. Too much release agent is used, or unsuitable release agent is used; <br> <br>B. The fluidity of the melt is poor, and it is easy to produce weld lines during molding; <br> <br>C. There is too much water in the raw material or the volatile content is too high. <br> <br>③ Forming operation: <br> <br>A. The melt temperature is too low, the low temperature melt has poor shunting and confluence performance, and it is easy to form weld lines; <br> <br>B. The melt injection pressure is too low, so that the injection speed is too slow, and the temperature of the melt in the cavity is not the same. At this time, the melt is easy to produce weld lines when the melt is divided and merged. <br> <br>As a reliable plastic molding company china, we can offer sorts of injection molded parts for sale, anything you need, please leave us a message.
About dgfeman com's Store
No description provided.
0.0
Customer Reviews
See what others are saying about dgfeman com's Store. We verify purchases to ensure reviews are genuine.
No reviews yet for this store.