Plumbing & Sanitary Repair
⚡ Hybrid Delivery
star
5.0 (0 Reviews)
0 Orders Completed
Precautions for Maintenance of Injection Moulding Dies

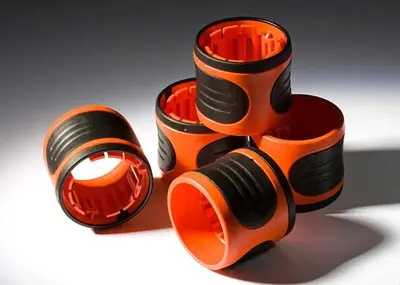
description Service Overview & Scope
The maintenance procedures required for each precision plastic injection moulding location depend on different mold cycles. Below are some general principles that every mold user can use to ensure the efficient operation of injection mold components such as hot runners, heaters, guide posts, and ejectors, in case the unexpected arises.
1. Check whether there is early-warning rust or moisture at the air diffuser of the injection moulding die
If you notice rust or moisture near the hot runner vents, it could mean condensation inside or possibly a ruptured water pipe. Moisture can cause a fatal short circuit to the heater. If the machine is not running all year round, but is shut down at night or on weekends, the chance of this condensation will increase.
2. Remember to remind the precision plastic injection moulding die operator not to "clean up" the hot nozzle at the gate
If the operator happens to see a small piece of stainless steel at the die runner, it may actually be a runner assembly. "Cleaning" out what appears to be a hindrance often destroys the hot tip. In order not to damage the hot nozzle, please confirm the nozzle type of the lower hot runner system before taking action, make sure that all operators are well trained and can recognize all the different nozzle types they come into contact with.
3. Sliding buckle of injection molding die
For machines that run year-round, this work should be done weekly.
4. The resistance value of the heater is checked interactively by the injection moulding die
You should have measured the resistance of your heater when you first started using it, now it's time to measure it again and compare. If the resistance value fluctuates by 10%, it is time to consider replacing the heater to ensure that it does not fail at a critical point in the production process. If the initial resistance value has never been measured, measure it now and use the resulting value as a reference for future inspections of the heater.
5. Check whether there are signs of wear between the guide post and the guide sleeve of the injection moulding die
Look for signs of scratches or scuffs, which are due to lack of lubrication. If the marks are just emerging, you can also extend the life of the guide posts and guide bushes by lubricating them more. If the wear is severe, it is time to replace the parts with new ones. Otherwise, the cavity and core parts may not fit well, resulting in different thicknesses of the part cavity walls.
6. Check the water flow during the production of the 2 shot plastic injection molding die
Connect a hose to the outlet of the waterway and let the water flow through the hose to the bucket. If the water flowing out is not clear or colored, rust may occur, and if the water is not flowing smoothly, it means that there is a blockage somewhere.
If these problems are found, re-drill all the water pipes to make sure they are clear (or clean them by whatever method you use most often). Improving the plant's water treatment system can prevent future problems caused by rust and blockages.
7. Clean the injection moulding die thimble
Over the course of a year, the thimble will become dirty due to gas build-up and film-like impurities. A good cleaning with mold cleaner every six to twelve months is recommended. After cleaning, apply a layer of lubricant to the thimble to prevent chafing or breaking.
8. Check whether there is a fracture in the radius area of the hot filling nozzle of the injection moulding die
Fractures are caused by loose hardened plastic fragments remaining in the hot nozzle of the machine from the clamping force from the injection barrel assembly during forward injection. It is also possible that the problem is caused by misalignment of the centerlines. Both possibilities are to be considered when finding fractures.
Sprue bushings should be replaced if the damage is severe enough to prevent petal-like leaks in the injection moulding die (referring to plastic leaks between the guide bush and the hot tip of the machine).
As one of 2k molding suppliers, we can offer sorts of related products for sale, anything you need, please contact us.
location_on
Service Coverage: Bangladesh
task_alt What's Included in this Service
check_circle
Service deliverables as requested
star Verified Client Reviews
Feedback from clients who completed orders on this service
5.0
star
star
star
star
star
0 ratings
star_border
No reviews yet. Be the first to order and share your feedback!
Service Fee / Price
From ৳0
Base rate — final quote depends on requirements
timer Turnaround:
⚡ 24 Hours
public Mode:
online
forum Response:
Within 1-2 Hours
chat
Send Direct Inquiry & Chat
Instant ordering & work tracker via EasyFIE Services Hub
Service Provider
dgfeman com verified
Member since Sep 2023
Official Storefront
storefront
dgfeman com's Store
shopping_bag
Book This Service
Order directly with verified milestone tracking
Service
Precautions for Maintenance of Injection Moulding Dies
Delivery Turnaround
⚡ 24 Hours
Total Service Fee
From ৳0
recommend Related Services You Might Like
 ⚡ 24 Hours
Plumbing & Sanitary Repair
gokul emexo
From ৳20,000
Details →
 ⚡ 24 Hours
Plumbing & Sanitary Repair
Pipe Relining Sydney | Sydney Relining Experts
From ৳0
Details →
 ⚡ 24 Hours
Plumbing & Sanitary Repair
Foot Valves
From ৳3,000
Details →
 ⚡ 24 Hours
Plumbing & Sanitary Repair
OEM Brass Ball Valves Factory
From ৳100
Details →